Skip to content


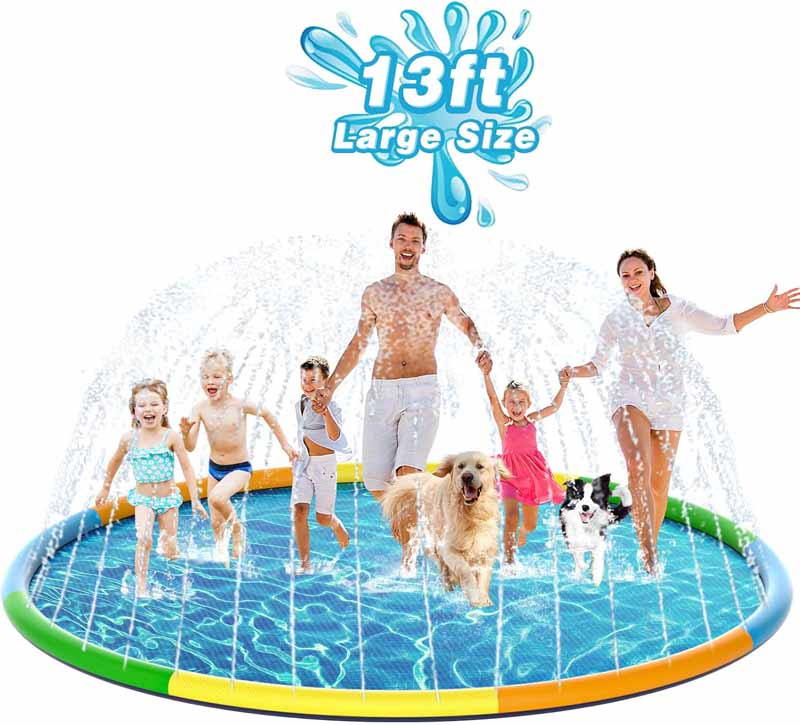
A custom dog splash pad may appear to be a printed PVC mat with a hose connector and a ring of spray holes, but reliable performance comes from dozens of connected decisions. The product has to remain manageable when folded, stable when wet, comfortable under paws, compatible with ordinary garden hoses, and strong enough for repeated setup, drainage, cleaning, and storage. A change in diameter, material thickness, channel width, hole count, or inlet position can influence spray balance, seam loading, packaging volume, production cost, and the way customers experience the finished product.
Custom dog splash pads are manufactured by defining the use conditions, converting those requirements into controlled drawings and material specifications, printing and cutting flexible PVC, welding a sealed perimeter water channel, installing the hose inlet, forming calibrated spray holes, testing the functional sample, approving production references, and transferring the verified design into bulk manufacturing. Reliable programs also control packaging, accessories, inspections, traceability, and future changes.
The most important work often becomes visible only after water enters the first sample. A design can look perfect when it lies flat on a table, yet the far side may spray weakly, the connector may twist under hose weight, or a fold line may cross a critical seam. Experienced manufacturers treat that first water test as an engineering conversation rather than a pass-or-fail ceremony. The following process explains how brands, retailers, importers, and product teams can turn a promising dog water-play idea into a practical product that can be produced again with consistent results.

What Must Be Defined Before Manufacturing Starts?
A custom dog splash pad should not enter development until the intended dogs, use environment, finished dimensions, water connection, spray expectations, surface requirements, target market, packaging, and quality criteria are clearly defined. These inputs determine the PVC construction, channel geometry, reinforcement, testing method, accessory set, production route, and whether the approved design can be reproduced consistently when the order moves from one sample to thousands of units.
Use Case and Dog Profile
The first decision is not the printed pattern. It is the job the product must perform. A compact pad designed for one small dog has different needs from a large model intended for several active dogs. Weight matters, but movement can matter just as much. A calm dog standing in shallow water creates less concentrated stress than a dog that repeatedly turns, scratches at moving jets, bites exposed parts, or jumps onto the wet center from outside the mat. Development teams should define dog size, expected activity, number of users, supervision, and whether children may share the product.
The setup environment also changes the risk profile. A pad used occasionally on a smooth patio does not face the same conditions as one placed daily on grass, compacted soil, decking, or a pet-care facility floor. Small stones, sharp twigs, exposed screws, rough concrete, and dirty surfaces can damage flexible PVC from underneath even when the top material is relatively heavy. A realistic product brief therefore includes ground preparation, expected cleaning frequency, seasonal storage, sunlight exposure, and the level of customer instruction needed to reduce avoidable punctures and surface wear.
Product Specification
Overall diameter is only one measurement. The perimeter water channel occupies part of the product, so the usable center area is smaller than the outside dimension shown on packaging. A product team should request both the finished outside diameter and the approximate inner play diameter. The specification should also identify the planned channel width, center-water depth under normal use, spray direction, connector location, folding method, packed size, and target weight. These values help prevent a visually impressive design from becoming difficult to ship, store, or use.
Water assumptions must be documented as well. Portable dog splash pads normally connect to a household garden hose, often through a standard 3/4-inch connection or an included adapter, but household flow varies with faucet condition, hose length, elevation, regional plumbing, and other water use at the property. The design should be tested across practical low, normal, and higher-flow conditions instead of relying on one ideal faucet. Product claims should describe adjustable spray through water pressure rather than guaranteeing one exact height in every home.
Customization Route
Customization can be divided into three practical levels. Private-label projects usually retain a proven structure while changing graphics, logo placement, Pantone colors, labels, instructions, barcodes, storage bags, repair accessories, and retail packaging. Platform modifications may change the diameter, outline, PVC construction, center texture, inlet position, spray-hole pattern, or local reinforcement. New development may introduce a different channel path, several spray zones, unusual shapes, combined pool-and-sprinkler functions, or new components that require additional engineering and process validation.
The lowest-risk route is not always the least creative route. A proven platform can still look highly distinctive when artwork, color blocking, packaging, accessories, and selected structural details are planned together. Full structural development is most useful when an existing platform cannot deliver the intended function or market position. Increasing the diameter, adding more holes, or relocating the inlet should never be treated as a simple drawing change because each adjustment may alter filling time, spray balance, seam stress, folding behavior, and carton size.
| Development Route | Typical Changes | Main Technical Risk | Appropriate Approval |
|---|---|---|---|
| Private Label | Logo, graphics, colors, labels, instructions, packaging | Artwork version or retail-file errors | Graphic sample plus packaging confirmation |
| Platform Modification | Diameter, texture, inlet, spray layout, PVC thickness | Changes to flow, seams, weight, or folding | Functional sample and repeated water testing |
| New Development | New channel, zones, attachments, combined functions | Higher tooling, process, and consistency risk | Feasibility review, revised samples, formal validation |
Commercial Constraints
A manufacturable product must also work inside the commercial plan. Larger diameters and heavier PVC can make the product feel more substantial, but they can also increase folded volume, retail-box size, carton weight, warehouse fees, and freight cost. An online marketplace may reward compact packaging, clear setup instructions, and a complete adapter set, while a retail chain may require shelf-ready dimensions, multilingual labeling, carton markings, and consistent visual presentation across several sizes. These requirements should be discussed before the sample is approved rather than added after production has started.
The project brief should include the target channel, destination market, expected order quantity, barcode system, packaging style, accessory list, instruction language, inspection expectations, launch timing, and repeat-order plan. EPN and its manufacturing platform commonly work with brands, retailers, importers, and online sellers that need visual customization combined with practical adjustments to structure, packaging, and accessories. The most dependable projects begin with a clear boundary between essential product features, preferred features, and changes that would add cost without improving the customer experience.

Which Materials and Structures Fit Dog Use?
Dog splash pads need a flexible PVC system that balances abrasion resistance, welding performance, wet-surface grip, print quality, foldability, product weight, and cost. Material thickness is important, but it cannot compensate for poor channel geometry, narrow seams, an unsupported connector, unsuitable texture, or weak quality control. The finished structure must be evaluated as one water-carrying product rather than as separate material and component specifications.
PVC Selection
For many portable dog splash pad projects, reinforced flexible PVC in an approximate 0.50 to 0.70 mm development range provides a practical starting point. This is not a universal requirement and should not be used as a shortcut for product engineering. A smaller supervised-use model may perform well with a lighter construction, while a large multi-dog version may need heavier material, selected reinforcement, or a different surface layer. The correct choice depends on diameter, intended activity, folding, price position, package limits, and the performance of the assembled sample.
Nominal thickness does not describe the complete material. Two sheets with the same measurement may differ in hardness, flexibility, plasticizer system, odor, surface finish, print adhesion, abrasion response, welding behavior, and recovery after folded storage. Material approval should therefore record the supplier code, nominal thickness, color, surface specification, intended component, printing method, and approved sample reference. Descriptions such as “heavy-duty PVC” are too broad to control future orders or explain differences between samples that look similar.
Surface and Wear
Wet grip is essential for dog use, but no flexible surface should be presented as completely slip-proof or claw-proof. Stability changes with dog speed, nail condition, water level, mud, soap residue, grass, surface wear, wrinkles, and the material underneath the pad. A moderate embossed or textured center can improve traction compared with a completely smooth film, yet deep embossing may reduce print clarity, trap dirt, slow drying, or create inconsistent contact if it extends into critical welding areas.
A practical structure may use a textured center while maintaining controlled flatter zones around the perimeter seal, connector flange, and other welded areas. Abrasion and puncture should also be treated as different problems. Abrasion develops through repeated paw movement, scratching, grit, folding, and cleaning. Puncture often occurs when a claw presses the PVC against a hidden stone or rough edge. Packaging and instructions should therefore explain the need for a clean, level setup surface, trimmed sharp nails, gradual water pressure, supervision, and complete drying before storage.
Water Channel
The outer ring is a hydraulic path rather than a decorative border. Channel width, perimeter length, inlet location, seam geometry, hole diameter, hole count, spacing, direction, and household flow determine how water moves around the product. A perfectly symmetrical drawing may still produce a weak far side if the route is too long or narrow. A channel that is too large may take excessive water and time to stabilize, while one that is too small may deform near the inlet and starve distant spray holes.
Spray holes should direct water inward toward the central play area and remain far enough from the welded seam to avoid weakening the edge. More holes do not automatically create a better experience. Adding holes divides the available flow and may reduce the height of every jet, especially on larger pads. Fewer holes may create stronger but less even streams. The target should be a balanced, adjustable spray pattern that works at practical household settings and remains comfortable for dogs with different confidence levels.
| Design Element | Common Development Reference | Main Verification Point |
|---|---|---|
| Main PVC | Approximately 0.50-0.70 mm for many dog-use platforms | Flexibility, abrasion, welding, odor, and fold recovery |
| Hose Connection | Commonly designed around a 3/4-inch garden-hose interface or adapter | Market compatibility, leakage, and ease of connection |
| Center Surface | Moderate embossing or selected texture | Wet grip, paw comfort, printing, cleaning, and drying |
| Water Channel | Sized according to diameter and expected household flow | Filling speed, shape stability, and far-side performance |
| Spray Holes | Controlled count, diameter, angle, and spacing | Inward spray, balanced distribution, and seam clearance |
| Reinforcement | Connector, transitions, and local stress areas | Strength improvement without excessive stiffness |
Inlet and Reinforcement
The hose inlet is one of the most stressed areas on a portable splash pad. It experiences internal water pressure, hose weight, twisting during connection, pulling when the hose moves, and repeated handling over the product’s life. A strong main sheet cannot compensate for an undersized flange or poorly supported fitting. The design may use a wider welded base, additional PVC layers, a sealing element, or a shaped reinforcement piece that spreads load into the surrounding material without creating a rigid edge.
Connector location affects both use and manufacturing. It should be accessible without encouraging users or dogs to step on it, and the hose should not cross the main play area. The fitting, thread, adapter, and reinforcement must be tested as the actual production combination. Repeated connection cycles are useful because some fittings pass an initial leak check but loosen after twisting. The final fold plan should also protect the inlet from being pressed into the printed center or forced across a hard crease inside the retail box.

How Is the Custom Sample Manufactured?
A custom sample is manufactured by converting the approved brief into controlled material, artwork, cutting, welding, component, spray-hole, and packaging files. The PVC is inspected, printed, cut, aligned, and heat sealed to form the water channel. The inlet and reinforcement are installed, holes are formed to a fixed layout, and the completed sample is cleaned, measured, water tested, revised, and formally approved.
Technical Files
Manufacturing should begin from a complete specification package rather than a collection of screenshots, voice messages, and old artwork attachments. The package should identify finished dimensions, usable center area, PVC codes, thickness, surface finish, artwork version, Pantone references, cut patterns, channel path, seam width, inlet type, spray-hole layout, reinforcement, accessories, labels, instructions, folding method, and packaging. Every file should carry a revision number so the production team can identify the current approved version.
A graphic sample and a functional sample answer different questions. A graphic sample can confirm logo placement, image scale, color direction, and general appearance. It cannot prove water distribution, seam strength, drainage, connector support, or folding behavior. When the diameter, material, channel, hole pattern, or inlet changes, a functional sample is required. Clear separation between visual approval and functional approval prevents a beautiful mock-up from being mistaken for a production-ready product.
Printing and Cutting
PVC sheets should be inspected before printing for material code, thickness, surface finish, color, contamination, wrinkles, and visible defects. Printing performance depends on the selected material and ink system, so adhesion, curing, registration, color consistency, fold response, and compatibility with later heat pressing should be reviewed. Important logos, faces, text, or detailed illustrations should remain clear of weld paths, connector flanges, and repeated fold lines where distortion or pressure marks are more likely.
Cutting converts approved digital patterns into the physical top panel, bottom panel, channel sections, reinforcement pieces, connector flanges, and other components. Small cutting differences can change the final diameter, seam overlap, hole location, and printed alignment across a long perimeter. Orientation marks can help operators match panels correctly, especially when graphics and inlet positions are not symmetrical, but those marks must be placed where they will not remain visible on the customer-facing product.
Welding and Assembly
Flexible PVC panels are commonly joined through high-frequency welding or another validated heat-sealing process suited to the material. Tooling shape, pressure, energy, time, material thickness, layer count, panel alignment, and cleanliness all influence the result. The tool creates the channel geometry, while the process must produce enough effective bonding area to withstand water pressure, repeated folding, and movement during use. Curves, tight transitions, multi-layer zones, and the inlet area require particularly careful control.
Operators should identify incomplete fusion, wrinkles, contamination, surface burning, shifted panels, narrow sealing areas, trapped air, and blocked channels before the product advances. The inlet is then assembled according to the approved orientation and reinforcement plan. Spray holes are formed only after the channel path and seam clearance are confirmed. A fixed template or controlled positioning method is preferable to visual estimation because small changes in hole size or angle become obvious when the pad is pressurized.
| Manufacturing Stage | Controlled Input | Typical Problem to Prevent |
|---|---|---|
| Material Release | Approved PVC code, thickness, finish, and lot | Wrong stiffness, color, odor, or welding response |
| Printing | Current artwork, color references, and orientation | Misregistration, weak adhesion, or wrong design version |
| Cutting | Approved dimensions, patterns, and panel direction | Reduced overlap, incorrect diameter, or shifted graphics |
| Welding | Tooling, settings, alignment, and surface cleanliness | Open seams, wrinkles, blocked channels, or burns |
| Inlet Assembly | Approved fitting, adapter, flange, and reinforcement | Leakage, twisting, poor hose fit, or sharp edges |
| Spray-Hole Formation | Fixed count, size, position, angle, and seam clearance | Uneven jets, outward spray, or weakened edges |
| Cleaning and Folding | Dryness, surface condition, accessories, and fold plan | Blocked holes, trapped moisture, or connector damage |
Sample Finishing
The assembled sample should be reviewed before water testing. Dimensions, artwork direction, seam continuity, connector position, hole layout, sharp trimming, exposed reinforcement, surface cleanliness, accessories, and folding method can all be checked while the product is dry. This step separates visible assembly problems from functional water-test findings and prevents time being wasted on testing a sample that already contains an obvious specification error.
Once water testing begins, observations should be connected to the exact sample version. Revisions must identify what is changing and what result is expected. “Improve the spray” is not a useful instruction; changing the hole diameter, reducing the count, moving the inlet, widening the channel, or adjusting the test pressure are different actions. EPN product development follows this practical sample-to-test cycle so artwork, structure, accessories, and packaging can be reviewed as parts of the same finished product rather than as isolated approvals.

How Is the Sample Tested Before Approval?
A dog splash pad sample should be approved as a complete working product, not only for color and appearance. Testing should cover filling behavior, spray distribution, leakage, connector stability, surface movement, controlled wear, drainage, drying, folding, accessories, packaging fit, and realistic use limits. Any change to the material, dimensions, water path, inlet, spray layout, or performance claim should trigger renewed functional evaluation.
Water Performance
Water should be introduced gradually while the sample lies on a clean, level surface and uses the intended production adapter. The team can observe filling speed, channel expansion, spray initiation, far-side response, ring twisting, outward movement, and visible leaks before the product reaches its normal operating shape. Testing only at one high faucet setting may hide weak low-flow performance or create an unrealistic result that customers cannot reproduce.
A practical test includes low, normal, and higher-flow conditions. At low flow, the channel should establish a usable spray without large dead zones. At the intended normal setting, jets should point toward the center with reasonable balance. At the higher condition, the ring should not bulge excessively, roll outward, expose stressed seams, or spray unpredictably beyond the play area. Useful records include stabilization time, approximate height at selected points, weak areas, inlet movement, visible deformation, and any change after several minutes of continuous use.
Seam and Connector
Leak testing should cover the full perimeter, tight curves, channel transitions, reinforced areas, inlet flange, and locations where several layers overlap. Some open areas leak immediately, while smaller defects begin to seep only after the channel has remained pressurized. The observation period should therefore be long enough to identify slow leakage rather than ending as soon as the first spray pattern appears satisfactory.
The inlet should be checked during connection, operation, hose movement, and disconnection. Technicians should look for dripping, fitting rotation, PVC distortion, flange lifting, stress whitening, or damage caused by the hose pulling from an angle. Repeated attachment cycles can reveal problems that one setup does not. After draining, the seam and connector area should be inspected again because local separation or permanent distortion may become more visible when the channel returns to its relaxed shape.
Dog-Use Evaluation
Dog-use evaluation should reflect normal supervised movement without pretending that one factory test can reproduce every animal’s behavior. Practical checks may include repeated walking, turning, light scratching, wet paw contact, edge entry, movement near the connector, surface marking, and local stretching. Comparative tests are most useful when two material or structural versions are exposed to the same contact method, wet condition, load, and cycle count, allowing the team to compare visible wear rather than making absolute claims.
The center should also be assessed for wrinkles, edge lifting, shifting, excessive pooling, and areas that become unusually slippery. Cleaning and drying are part of performance because hair, grass, mud, and outdoor debris often remain after play. The surface should be reasonably easy to rinse, and the structure should not create deep pockets that retain water. The product should be completely dry before folding; trapped moisture can lead to odor, marks, packaging damage, and poor customer impressions even when the water system itself works correctly.
Approval Record
Approval should be written and tied to a clearly identified physical sample or production-equivalent reference. The record should include dimensions, material codes, surface finish, artwork version, seam layout, inlet, spray pattern, accessories, warnings, folding method, packaging, and agreed tolerances. A Golden Sample is valuable, but it cannot replace technical files because two materials may look similar while differing in formulation, welding behavior, odor, or long-term fold recovery.
Known limits should be recorded with successful results. Spray height depends on household flow. Wet grip changes with contamination, movement, and setup surface. Puncture resistance depends partly on ground preparation and dog behavior. Clear limits make product claims more credible and reduce disputes after launch. They also help customer-service teams give useful setup guidance rather than treating every damaged product as either misuse or a manufacturing defect without examining the conditions.
| Approval Area | Evidence to Keep | Core Acceptance Question |
|---|---|---|
| Appearance | Approved sample and artwork revision | Are graphics, colors, and positions correct? |
| Dimensions | Drawing and measured sample record | Is the outside size and usable center within tolerance? |
| Materials | PVC, ink, fitting, and component codes | Is the approved construction locked for production? |
| Water Function | Low, normal, and higher-flow observations | Does the product fill, spray, and remain stable? |
| Leak Resistance | Seam and inlet test record | Are critical welded and fitted areas dry? |
| Dog-Use Performance | Controlled surface and movement observations | Do claims match realistic supervised conditions? |
| Packaging | Packed sample, accessory list, and label files | Will customers receive a complete, dry, usable product? |

How Does an Approved Sample Reach Bulk Production?
An approved sample reaches bulk production through a controlled transfer of materials, artwork, drawings, tooling references, components, process settings, inspection points, packaging files, and functional-test requirements. Consistency depends on first-article approval, incoming inspection, in-process checks, final sampling, traceability, and formal change control rather than asking production teams to reproduce a sample from memory or appearance alone.
Production Transfer
Before bulk materials are released, the development package must become clear production instructions. The bill of materials should identify the exact PVC, ink or printing system, reinforcement, fitting, adapter, repair patch, storage bag, instructions, labels, retail box, and shipping carton. Drawings should show panel orientation, channel path, seam width, connector position, spray-hole layout, and critical dimensions. Artwork must be locked to the correct size, language, barcode, SKU, and sales channel so similar versions are not mixed.
A first production article provides an important checkpoint. It confirms that bulk material lots, actual tooling, line operators, process settings, and the packing method can reproduce the approved sample. This is particularly important when the development unit was built slowly by an experienced technician but the order will be produced through repeated line operations. Warm-weather products also have a limited selling window, so material booking, artwork approval, packaging delivery, inspection, and shipping need to be coordinated rather than managed as unrelated deadlines.
In-Process Control
Quality control should begin before assembly. Incoming checks confirm that the PVC, fittings, adapters, accessories, boxes, and labels match the released specification. Printing inspection catches color, registration, curing, surface marks, and version errors before the material is converted. Cutting inspection verifies dimensions, orientation, clean edges, and correct grouping by SKU. These early checks are less expensive and more reliable than finding a mixed material or wrong artwork after hundreds of products have already been welded.
During heat pressing, inspectors review alignment, seam continuity, channel shape, pressure marks, wrinkles, contamination, reinforcement position, and local overheating. Inlet assembly and spray-hole formation require their own controls because a product can look visually acceptable while leaking or spraying unevenly. Inspection frequency should reflect order size, process stability, product complexity, and previous results. First articles, routine samples, and units showing abnormal seams or deformation should receive water testing under the agreed method.
Final Inspection and Packing
Finished-product inspection should cover appearance, dimensions, seams, inlet assembly, hole layout, surface cleanliness, accessories, labels, folding, and packaging. Selected units should be functionally tested according to the agreed sampling plan. Products must then be fully drained and dried before packing. Moisture trapped inside folds or channels can produce odor, marks, packaging damage, or customer concern, so drying is a production requirement rather than a cosmetic finishing step.
The folding method should keep hard creases away from critical seams and protect the connector from pressing into the printed center. Accessory counting deserves equal attention. A missing adapter or instruction sheet may make an otherwise acceptable product difficult to use. Retail boxes and shipping cartons should be checked for dimensions, weight, quantity, barcode accuracy, markings, closure, and internal movement. E-commerce parcels face repeated individual handling, while wholesale cartons may move on pallets, so packaging must match the actual distribution route.
Repeat Orders and Change Control
Repeat-order consistency depends on records rather than memory. Production should return to the approved material codes, artwork, drawings, Golden Sample, component references, packing files, inspection criteria, and quality history. A replacement PVC sheet or fitting should not be accepted only because it looks similar. Differences in hardness, surface finish, formulation, geometry, ink compatibility, or welding response can affect spray balance, seam strength, odor, folding, and customer setup.
Any proposed change that may influence function, appearance, compliance, packaging, or use should be reviewed before production. Previous order data also deserves attention. If earlier runs showed recurring weak spray at one point, minor inlet seepage, fold marks, missing accessories, or carton damage, the next order should include targeted controls. Stable manufacturing does not mean every flexible product will be visually identical in every minor detail. It means critical characteristics remain within agreed limits and abnormal changes are detected before they become market problems.
Conclusion
Custom dog splash pad manufacturing is most successful when the product is treated as a connected system rather than a printed PVC item with a few added components. The dog profile influences the usable area and surface. The diameter affects the water route and packaging. The material affects printing, welding, wear, folding, and odor. The channel and spray holes determine water performance, while the inlet, seams, drying method, and accessory set influence the customer’s experience long after the product leaves the factory.
For brands and retailers, the strongest sign of manufacturing capability is a traceable process. A dependable supplier asks specific questions, explains trade-offs, locks material and component codes, builds a functional sample, records water and use observations, approves the complete package, and carries those references into bulk production and repeat orders. EPN’s work with welded PVC recreational products brings product development, manufacturing, consumer use, packaging, and seasonal sales considerations into the same conversation, helping custom projects remain practical from the first drawing through the final packed carton.
Frequently Asked Questions
What PVC thickness is suitable for a dog splash pad?
Many portable dog splash pad projects begin development around 0.50 to 0.70 mm flexible PVC, but the correct construction depends on diameter, dog activity, surface design, folding requirements, reinforcement, price position, and sample results. Thickness should be evaluated together with material formulation, welding performance, abrasion response, odor, packed volume, and the ground conditions expected during use.
How long does a custom dog splash pad take to manufacture?
Timing depends on whether the project uses private-label graphics, modifies an existing structure, or requires new tooling and repeated functional samples. Artwork approval, material availability, sample revisions, packaging development, testing, order size, seasonal factory capacity, and shipping method all influence the schedule. A realistic plan separates sample lead time, approval time, bulk production, inspection, and transportation instead of combining them into one unsupported promise.
Can spray height be customized?
Spray height can be influenced by hole diameter, hole count, hole angle, channel size, pad diameter, inlet position, and household water flow. Manufacturers can develop a preferred pattern and test it at several practical flow conditions, but one exact height cannot be guaranteed for every property. The most practical design allows users to begin with low pressure and adjust the faucet gradually for the dog’s comfort.
Are custom dog splash pads completely claw-proof?
No flexible PVC splash pad should be described as completely claw-proof. Material selection, texture, reinforcement, clean setup surfaces, and controlled wear testing can improve resistance to normal supervised paw contact, but sharp nails, deliberate digging, biting, and hidden stones can still damage the product. Credible product information explains these limits and provides setup, supervision, inspection, cleaning, repair, and storage guidance.
What should be checked before approving a sample?
Approval should cover the finished dimensions, usable center area, PVC and component codes, graphics, seam layout, inlet, spray-hole pattern, low-to-higher-flow performance, leakage, surface behavior, drainage, drying, folding, accessories, labels, instructions, and packaging. The physical sample should be linked to controlled drawings, artwork, test records, and revision numbers so the factory can reproduce the same approved construction in bulk.
How can repeat production remain consistent?
Consistency comes from locked specifications, approved material and component codes, a Golden Sample, controlled artwork, first-article checks, in-process inspection, functional sampling, packing verification, traceability, and formal change control. Previous quality findings should also be reviewed before each new order. A supplier substitution or process adjustment should be evaluated whenever it could affect appearance, welding, water flow, odor, folding, compliance, or customer setup.